
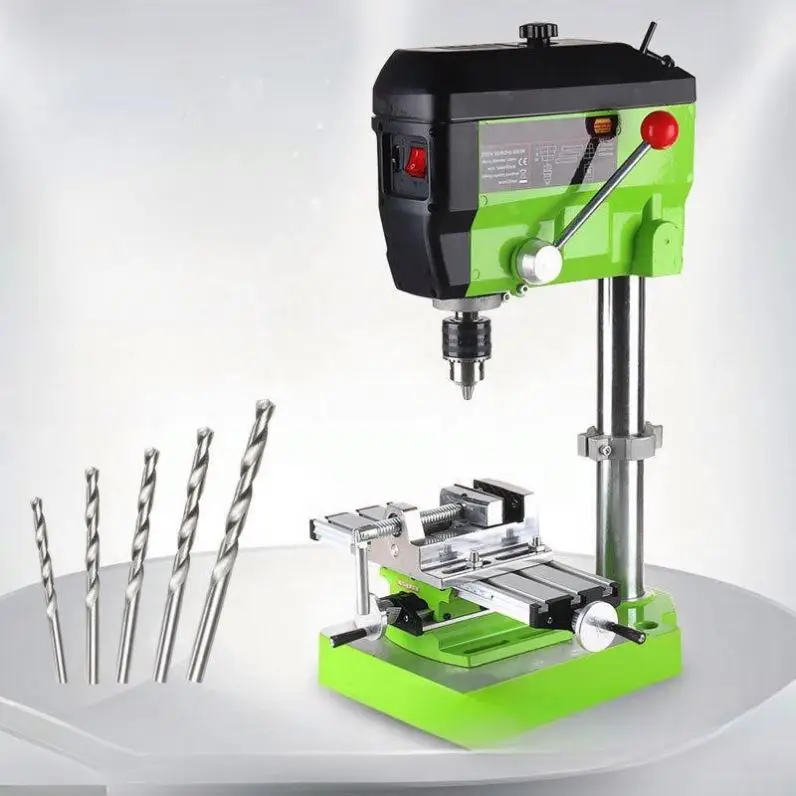
Source-controlled product identity
The Hoting queue record identifies this product as a Bench Drill, while the listing title positions it as a miniature milling machine with a bench vise, fixture worktable and X/Y-axis adjustment coordinate table. The structured source fields provide: 220V, 50-60Hz, 710W, 0-2800R/MIN no-load speed, 60mm stroke length, 110mm working radius and 1.5-13mm clamping capacity. The source application covers metal, wood boards and plastic materials.
Those values establish the recorded bench-drill configuration. They do not establish milling capability, X-axis travel, Y-axis travel, table accuracy, vise jaw size, spindle taper, cutter compatibility, lateral cutting force, machine weight, table dimensions or a precision tolerance. The title claims must therefore be verified separately before the unit is purchased for milling or coordinate work.
Product ID 1601276901987 should appear on the quotation, nameplate, datasheet, inspection report and packing list. This guide is written for buyers deciding whether the product is suitable as a drill, a guided drilling fixture or a light-duty coordinate workholding setup. It should not be used as proof that the unit is a production milling machine.
Recorded specifications versus title claims
| Information | Source status | Procurement requirement |
|---|---|---|
| Product Name | Bench Drill | Confirm the exact model and whether the quoted coordinate table and vise are included or optional. |
| Voltage | 220V | Confirm phase, tolerance, plug, current, earthing and destination configuration. |
| Frequency | 50-60Hz | Confirm motor behavior and speed/thermal limits at both frequencies. |
| Power | 710W | Clarify input versus output power and obtain rated-load data. |
| No-load Speed | 0-2800R/MIN | Confirm control method, speed settings and loaded speed; do not treat it as milling speed. |
| Stroke Length | 60mm | Confirm quill/spindle travel and depth-stop repeatability. |
| Working Radius | 110mm | Confirm the measurement reference and usable throat after fitting the table and vise. |
| Clamping Capacity | 1.5-13mm | Confirm chuck type, runout and tool-shank range. |
| Application | Metal, wood boards and plastic materials | Request material-specific drilling settings and sample results. |
| X/Y coordinate table | Title claim, no structured dimensions | Request X/Y travel, screw pitch, backlash, table size, slots, locks and repeatability. |
| Miniature milling machine | Title claim, not a recorded product name | Require a separate milling capability statement, cutter range, lateral-load limit and test. |
| Bench vise/fixture | Title claim, no jaw or travel data | Confirm jaw width, opening, height, mounting, accuracy and inclusion in the quote. |
Decide whether the need is drilling or milling
A bench drill is primarily a vertical drilling machine: the tool rotates and the feed is normally axial. Milling introduces lateral cutting loads, cutter side force, tool deflection and workholding requirements that are not established by a drill’s voltage, power or chuck range.
Write the required process before comparing this listing. If the job is hole drilling, define hole diameter, depth, material, bit type, tolerance, position and repeatability. If the job is slotting, facing, edge milling or pocketing, define cutter diameter, material removal, depth of cut, lateral load, coordinate travel and surface-finish target.
Do not use the phrase “miniature milling machine” as a substitute for a documented milling rating. Ask the supplier whether the motor, spindle, bearings, chuck and frame are approved for lateral cutting. Request a demonstration using the buyer’s material and cutter, not only an unloaded spindle test.
For occasional guided drilling, the coordinate table may be useful as a positioning fixture. For continuous milling, the buyer should require a dedicated machine specification or a written limitation that clearly excludes milling.
Electrical and motor verification
The source records 220V, 50-60Hz and 710W. Request the exact nameplate, wiring diagram, plug, cable length, phase, rated current, start-up current and protective-device recommendation. Confirm whether the machine has a single motor configuration across the destination voltage and frequency range.
Clarify whether 710W is input power, rated motor output or maximum consumption. Test the machine at the buyer’s supply with the intended bit and workpiece. Record current, speed stability, housing temperature, vibration and switch behavior under load.
Ask how the machine responds to a stalled bit or lateral cutter load. Confirm overload, thermal protection, restart prevention and the safe method for stopping rotation. A power-off switch is useful, but it does not by itself prove overload protection for milling.
If the supplier offers different speed or motor versions, require separate model numbers and nameplates. The quotation must identify the exact electrical configuration, not only the shared product title.
Speed range and tool selection
The recorded no-load speed is 0-2800R/MIN. Request the control method, minimum stable speed, number of settings, display or scale and loaded-speed data at representative drilling conditions.
For drilling, choose speed from material, bit diameter and bit material. For any proposed milling operation, request a separate cutter-speed chart and state whether the values are allowed under lateral load. Do not assume that a high no-load speed is suitable for a large cutter or hard material.
Measure the spindle speed with a calibrated tachometer or the supplier’s documented method. Record the selected setting, measured no-load speed and loaded speed. Repeat after the machine reaches normal operating temperature to identify drift.
Confirm whether the 1.5-13mm clamping capacity refers to a drill chuck. A chuck may hold a shank, but it does not automatically provide the rigidity or concentricity required for side milling. Ask for spindle interface, chuck runout and an explicit statement about permitted tool types.
60mm stroke and vertical travel
The source records a 60mm stroke length. Confirm whether this means quill travel, spindle travel or another vertical movement. Request a dimensioned drawing, depth-stop range, scale resolution and repeatability.
Measure the usable travel with the selected chuck, holder and tool installed. The 60mm value does not establish available hole depth because tool length, workpiece height, table position and chuck clearance also matter.
For coordinate drilling, test repeated holes at different table positions while keeping the vertical stop fixed. Record hole depth variation and the effect of locking the quill, table and coordinate screws.
If a supplier proposes milling, request the maximum vertical cutter reach and depth-of-cut procedure. A drill’s vertical stroke should not be treated as a milling depth rating.
110mm working radius and coordinate-table envelope
The source records a 110mm working radius but does not define the reference point. Request a drawing showing spindle centerline to column, usable throat, table boundaries and clearance after installing the vise or coordinate table.
Ask separately for X travel and Y travel. These values are absent from the source record and must not be inferred from the title or product images. Request screw pitch, scale resolution, backlash, locking method, table flatness and repeatability.
Map the usable work envelope using the actual chuck, tool, fixture and workpiece. A coordinate table can reduce the available working radius or vertical clearance, especially when a vise is mounted on top of it.
Test hole-position repeatability by moving the table away and back to a reference. Record direction, screw backlash, lock sequence and measured coordinate error. Use the buyer’s actual tolerance rather than a visual alignment judgment.
Vise, fixture and workholding requirements
The title mentions a bench vise and fixture, but no jaw width, opening, height, travel, material or accuracy is provided. Request a complete accessory list and a drawing of the mounting slots or bolt pattern.
Measure jaw parallelism, jaw opening and clamping height. Confirm that the vise can hold the buyer’s smallest and largest workpieces without interfering with the chuck, column or depth stop.
For drilling, check that the workpiece is supported close to the hole and cannot rotate. For any lateral cutting proposal, check that the fixture resists side force without shifting. A small vise can position a part but may not be adequate for a milling load.
Ask whether soft jaws, step clamps, T-slots or custom fixtures are included. Accessories visible in listing images may be optional; only the written quotation and packing list should define the delivered package.
Coordinate accuracy and backlash acceptance
Set measurable acceptance criteria for the X/Y table before purchase. Specify table travel, coordinate resolution, backlash, repeatability, hole-position error over the working area and the locking sequence used during drilling.
Use a reference plate or calibrated test grid. Drill a pattern at defined coordinates, measure center-to-center distances and compare the result with the buyer’s tolerance. Repeat after returning the table to the origin and after changing direction on each axis.
Record whether the table moves smoothly across its full range. Inspect lead screws, nuts, guides, locks, gib adjustment and end stops. Ask for the maintenance procedure and replacement parts for worn screws or nuts.
Do not claim CNC-like accuracy from a manual coordinate table. The buyer should describe it as a manual positioning aid unless the supplier supplies a tested tolerance under defined conditions.
Material-specific drilling checks
The application field lists metal, wood boards and plastic materials. The description also mentions aluminum, composite panels, resin panels, thin metal, circuit boards and hard materials. These are application statements, not a full capacity chart.
Request separate recommendations for mild steel, stainless steel, aluminum, wood, plastic and composite materials. Define bit material, point geometry, speed, feed, lubricant, pecking cycle, hole diameter and allowable burr or surface damage.
For plastic, test melting, edge breakout and chip evacuation. For wood, test tear-out and workpiece movement. For metal, inspect burrs, hole roundness, work hardening and heat. For composites or circuit boards, clarify dust control and tooling limits.
Use a sample report that identifies the material and tool. A statement that the machine is “widely used” does not prove the buyer’s required tolerance or cycle time.
Milling-specific risk review
If the buyer intends to mill, obtain a written answer to five questions: Is side milling permitted? What cutter types and maximum diameters are allowed? What lateral load or depth of cut is permitted? What spindle interface and runout are guaranteed? What workholding and guard are required?
Run a controlled test with a small cutter and the buyer’s material only after the supplier confirms the configuration. Record cutter diameter, speed, feed, depth of cut, lateral engagement, current, vibration, deflection, finish and tool retention.
Stop the test if the workpiece shifts, the chuck slips, the spindle deflects, the frame vibrates excessively or the motor overheats. A successful light scratch does not demonstrate production milling capacity.
If the supplier cannot document lateral-load limits, keep the purchase scope to drilling and coordinate positioning. This protects the buyer from converting a title claim into an unsupported machine rating.
Table, base and installation
The source record does not provide overall dimensions, table size, base footprint, column diameter, mounting holes or weight. Request a dimensioned installation drawing before selecting a bench or stand.
Check table flatness, slot layout, tilt, height adjustment and locking. Test the frame with the intended workpiece clamped and the table at the outer limits of its travel. Record movement, vibration and deflection.
Leave clearance for the chuck, tool, guard, vise, coordinate screws, handles, cable and long stock. The title’s “miniature” wording does not establish the complete operating envelope.
Confirm whether the machine requires anchoring. If so, request bolt size, hole spacing, support thickness and a safe method for leveling the base.
Safety and documentation
Request the instruction manual and risk warnings for the exact Bench Drill configuration. Inspect rotating parts, chuck, guard, gear housing, table locks, coordinate screws, vise and power switch.
Confirm restart prevention after a power interruption. Test the power-off control and verify that the operator can isolate power before changing tools, clearing chips or adjusting the fixture.
Keep hands clear of rotating tools and moving table screws. Clamp the workpiece; do not hold it by hand during drilling. Long stock should be supported so it cannot swing or rotate.
If milling is proposed, require additional safety instructions for side loads, cutter retention, chip direction, workholding and maximum engagement. No product-level certification is supplied in the source record, so request destination-market documents for the exact model and configuration.
Factory acceptance test proposal
- Verify product ID 1601276901987, Bench Drill model, nameplate, 220V, 50-60Hz and 710W definition.
- Test plug, earth, cable, switch, power-off behavior, restart prevention and protective-device requirements.
- Measure no-load speed across the documented range and record loaded speed under an agreed drilling condition.
- Verify 60mm vertical stroke, depth stop, scale, lock and repeatability with the buyer’s tool.
- Confirm the 110mm working-radius reference and usable clearance after installing the table and vise.
- Measure 1.5-13mm chuck capacity, runout, tool retention and bit release.
- Verify X/Y table travel, screw pitch, backlash, locks, flatness, vise dimensions and positioning repeatability.
- Drill metal, wood and plastic samples using agreed tools, speeds, feeds, lubricants and tolerances.
- If milling is requested, conduct a separately approved light-load test and record all lateral-load conditions.
- Review accessories, installation drawing, manual, safety documents, packing, warranty, MOQ and lead time.
RFQ checklist
- Product ID 1601276901987, exact model, nameplate photograph and current datasheet.
- 220V configuration: phase, tolerance, current, plug, cable, earth, fuse and breaker requirement.
- 50-60Hz operation: motor behavior, permitted range, speed and thermal test conditions.
- 710W definition: input/output power, current, start-up current and duty cycle.
- 0-2800R/MIN control method, speed settings, loaded speed, accuracy and minimum usable speed.
- 60mm stroke: quill/spindle reference, depth stop, scale, lock and repeatability.
- 110mm working radius: drawing reference, throat, clearance and coordinate-table envelope.
- 1.5-13mm chuck: type, interface, runout, key, jaw range and permitted tooling.
- X travel, Y travel, table dimensions, screw pitch, backlash, locks, flatness and repeatability.
- Vise details: jaw width, opening, height, travel, mounting, parallelism and inclusion status.
- Explicit statement on whether side milling is permitted, with cutter, lateral-load and depth limits.
- Material-specific drilling data for metal, wood, plastic, aluminum, composites and circuit boards.
- Overall dimensions, base, column, weight, installation, guards, manual and compliance documents.
- MOQ, sample cost, lead time, warranty, spare parts, service contact and inspection terms.
Buyer decision framework
This listing is a starting point for sourcing a 220V bench drill with a possible coordinate-table and vise configuration. The source-backed values are 220V, 50-60Hz, 710W, 0-2800R/MIN no-load speed, 60mm stroke, 110mm working radius, 1.5-13mm clamping capacity and the stated material applications. Approve it as a drilling and positioning tool only after the supplier confirms the accessories, coordinate travel, chuck runout, work envelope and drilling results. Approve any milling use only after a separate written capability statement and controlled lateral-load test.
Frequently asked questions
Is this definitely a milling machine?
The title uses “miniature milling machine,” but the structured Product Name is Bench Drill. Request explicit milling capability, cutter limits and lateral-load data before using it for milling.
What are the X and Y travel distances?
The source record does not provide X or Y travel. Ask for a dimensioned coordinate-table drawing and verify travel, backlash and repeatability.
Can the 1.5-13mm chuck hold milling cutters?
The source records a clamping capacity but not permitted cutter types or spindle rigidity. Confirm tool compatibility and side-load limits in writing.
What materials can be drilled?
The application field lists metal, wood boards and plastic materials. Request a material-specific drilling chart and test the buyer’s actual stock.
Does the 60mm stroke define hole depth?
No. It is a recorded stroke value. Tool length, workpiece height, table position and chuck clearance also determine usable hole depth.
Source and contact
This guide is based on the Hoting queue record for product ID 1601276901987. Before purchase, request the current quotation, electrical datasheet, coordinate-table drawing, vise and chuck details, drilling chart, milling capability statement if needed, safety manual, packing list, spare-parts offer, warranty and final machine photographs. For sourcing questions, contact the TEBAK sales team through the site’s current inquiry channel.
Key specifications
- Product Name
- Bench Drill
- Voltage
- 220V
- No-load Speed
- 0-2800R/MIN
- Frequency
- 50-60Hz
- Power
- 710W
- Stroke Length
- 60mm
- Working Radius
- 110mm
- Clamping Capacity
- 1.5-13mm
- Application
- Can be widely used metal, wood boards, plastic materials, etc.
- Feature
- Gear drive, power-off switch and multipurpose bench drilling claims; verify X/Y table and milling configuration.